Ohsure’s Activewear Quality Control Process Explained Step by Step
Quality-control process guide · Sources reviewed October 7, 2026
Direct answer: Ohsurewear describes a staged quality process: inspect incoming fabric, verify construction and fit through samples, control cutting and sewing during bulk production, then inspect finished garments and packing. For a buyer, each gate should use the approved specification, record results by lot or order, identify nonconformities and require written disposition before production advances.
Quality is not proven by a final inspection alone. Fabric variation, an unapproved pattern change or a repeated sewing defect can affect an entire order before finished goods exist. The useful control is a chain of evidence that links the buyer's requirement to the material lot, approved sample, production checkpoints and shipment decision.
What Does Ohsure's Published Quality Process Cover?
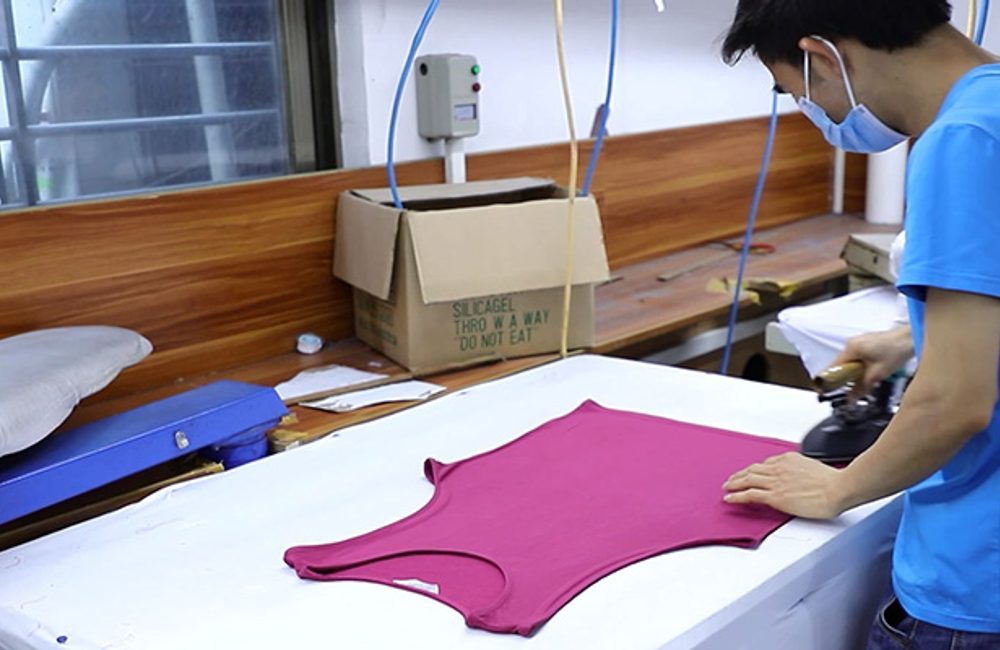
Ohsurewear's quality-control page presents four operating stages: raw-material control, cutting and printing inspection, semi-finished-product sampling inspection, and finished-product testing. Its manufacturing page also describes fabric inspection, sample revisions before approval and in-line production checks.
These pages describe the workflow, but a buyer still needs order-specific acceptance criteria. Words such as “good,” “consistent” and “durable” should be converted into a test method, tolerance, approved reference or defect rule before sampling and bulk production begin.
The Step-by-Step Handover: Who Checks, Records and Releases?
The seven steps below turn the published production stages into a recommended order-control workflow. The role names are responsibilities to assign at project kickoff, not a claim about Ohsure’s internal job titles or a verified factory SOP. One person may fill more than one role, but an approval must identify its authorized owner.
| Step / timing | Suggested responsibility | Required action | Handover record |
|---|---|---|---|
| 1. Agree the order standard Before material release | Buyer technical lead + supplier project contact | Confirm tech-pack revision, measurement method, tolerances, approved components and artwork. Name who can approve a deviation. | Approved specification and inspection plan |
| 2. Release incoming materials Before cutting | Material inspector + designated QC approver | Identify rolls and dye lots, compare shade references, record width and GSM, and link required tests. Segregate suspect material. | Material inspection and lot disposition |
| 3. Approve the production reference Before bulk starts | Sample team + buyer approver | Close fit and construction comments. Identify the sealed sample and confirm whether its fabric, trims and decoration represent bulk. | Dated approval with revision and open-item status |
| 4. Verify first production output At cutting, decoration and sewing setup | Production supervisor + QC inspector | Check the first output after setup or a relevant change. Compare panels, placement, seams and measurements with the released references. | First-piece result and restart authorization |
| 5. Monitor and contain defects During production | Line inspector + operation owner | Record inspection coverage and defects. Trace affected bundles, isolate suspect output, correct the operation and document a recheck. | In-line log and corrective-action record |
| 6. Decide final lot acceptance At the agreed inspection readiness | Final inspector + designated release authority | Inspect the defined lot under the agreed plan. Reconcile measurements, defect counts, required tests, quantities and packing. | Final report and acceptance decision |
| 7. Authorize dispatch and retain evidence After inspection closure | Shipment coordinator + release authority | Match released quantities to cartons and the packing list. Confirm closed holds and written release before dispatch. | Shipment release and retained order dossier |
Set a reporting schedule and an escalation contact before production. A daily progress photo can support communication, but it does not replace a measurement sheet, lot-linked inspection result or written release. Keep the same purchase-order and style identifiers across every handover.
The Quality Gate Matrix: What Must Be Approved Before Moving Forward?
| Gate | Control basis | Typical evidence | Stop or release decision |
|---|---|---|---|
| 1. Incoming fabric and trims | Purchase specification, approved swatch, color standard and required tests | Lot identity, width/GSM readings, shade review, defect record and relevant test report | Quarantine, replace, conditionally accept or release to cutting |
| 2. Development sample | Tech pack, measurement chart, artwork and construction notes | Measurement sheet, fit comments, photographs and revision list | Revise or advance to size set / pre-production sample |
| 3. Pre-production approval | Final specification and all approved components | Signed or traceable approval, sealed sample, color and trim references | Do not start bulk without approval and resolved deviations |
| 4. Cutting, printing and sewing | Approved sample, workmanship standard and tolerances | First-piece check, in-line inspection log, defect trend and corrective action | Correct the process before the defect spreads |
| 5. Finished goods and packing | PO, size specification, labeling, packing and inspection plan | Final inspection report, quantity/SKU check, test results and release record | Rework, sort, reinspect, accept by concession or release shipment |
Gate 1: How Fabric and Trims Are Verified
Ohsurewear states that fabric is checked before production for specification, color consistency and performance characteristics. Its QC page lists color difference, weight, pilling or fuzzing, colorfastness, puncture resistance and shrinkage among the fabric-control topics shown.
The actual test plan should depend on the garment and claim. Leggings may prioritize GSM, stretch and recovery, opacity, colorfastness and shrinkage; a jacket may add coating, water-resistance or zipper checks; brushed fabric may require special attention to pilling and hand feel. A supplier certificate should be matched to the actual composition, color and production lot rather than accepted as a generic promise.
- Identify the lot: record supplier, composition, color, roll or batch and arrival date.
- Define the method: specify units, conditioning, equipment and pass/fail limits.
- Control shade: compare rolls and approved references under agreed lighting.
- Separate failures: label and quarantine material until disposition is authorized.
- Preserve traceability: link released material to the cutting and production order.
Gates 2 and 3: From First Sample to a Controlled Bulk Standard
A sample is useful only when its status is clear. A first prototype explores the design; a fit sample resolves shape and measurement; a size set checks grading; and a pre-production sample should represent the final material, trims, artwork and construction intended for bulk. Names vary, so the purchase order should define each approval gate.
Ohsurewear's published process says pattern making and sample development are used to validate fit, structure and construction, with feedback addressed through revisions until approval. The approved sample should be paired with the latest tech pack and a closed change log. If a bulk material, color, trim or process differs from the approved sample, the deviation should be disclosed and approved in writing.
A usable sample approval record
- Style, version, size and date
- Measurements with actual results and tolerances
- Fabric, trim, color and artwork references
- Open comments, corrections and agreed deviations
- Clear status: rejected, revise, conditionally approved or approved
- Approver identity and the files or physical sample that become the bulk standard
Gate 4: How In-Line Checks Protect Bulk Production
Ohsurewear says it performs checks during garment making rather than waiting until the end. Its public QC description focuses on sewing-thread uniformity, skipped or broken stitches, seam density, wrinkles, firmness and loose threads. The manufacturing page adds stitching, sizing and construction checks.
An effective in-line check uses early production pieces and recurring samples to detect a trend. Inspectors should record the operation, size, defect, quantity checked, quantity failed, root cause, corrective action and recheck result. A repeated seam failure should trigger machine, needle, thread, tension or operator review—not simply trimming the visible symptom.
Cutting drift
Compare markers, notches, ply alignment and cut panels to the approved pattern before bundles reach sewing.
Print or logo error
Check color, position, dimensions, adhesion and appearance against approved artwork and test requirements.
Seam inconsistency
Check stitch type, density, stretch, tension, skipped stitches and seam appearance at the operation producing the risk.
Measurement trend
Measure selected points across sizes and times; investigate drift before it becomes a full-lot issue.
Gate 5: Finished-Garment Inspection and Shipment Release
Ohsurewear's published final checks include appearance, dimensions, loose threads, sewing, accessories and detailed functional items such as buttons and zippers. The order's final plan should also cover assortment, labels, barcodes, packaging, carton quantity and any required product testing.
Final inspection is a release decision, not proof that earlier controls were unnecessary. The buyer and supplier should agree whether inspection is 100%, risk-based or sampling-based; which defects are critical, major or minor; and what happens after a failure. If AQL sampling is used, state the sampling standard, lot definition, inspection level, AQL by defect class and reinspection rule. Do not assume a generic “AQL 2.5” phrase defines the whole plan.
How to Handle a Failed Check: Three Worked Examples
These are illustrative control scenarios, not Ohsure customer cases or reported factory results. Defect severity must follow the approved defect catalogue and product risk.
| Observed issue | Containment and investigation | Evidence needed to close |
|---|---|---|
| Shade difference between cut panels | Hold the affected bundles; trace roll and dye-lot identities. Compare panels with the approved shade reference under the agreed viewing conditions. | Record affected quantities, shade groups, replacement or sorting action, reinspection results and the authorized disposition. |
| Skipped stitches at a leggings seam | Hold output from the affected operation since the last verified acceptable checkpoint. Examine setup, needle, thread, tension and handling before restarting. | Retain defect photos, operation and time references, the correction, and new seam checks under the agreed extension conditions. |
| Waist measurement outside tolerance | Confirm the measurement method and instrument first. Trace sizes, bundles and time period; investigate pattern, cutting and sewing contributions. | Record actual measurements before and after correction, the extent of affected stock, rework results and written release. |
Correcting the first defective piece does not close the event. Establish the affected population, decide how it will be checked, and verify both corrected stock and newly produced output. A concession must describe its exact scope and approver; it does not automatically change the specification for future orders.
How the Final Inspection and Test Records Should Be Written
If the order uses acceptance sampling, record the agreed standard and edition. ISO 2859-1:2026 describes AQL-indexed sampling schemes for lot-by-lot inspection by attributes. Its publication does not establish which edition or plan Ohsure uses for a particular purchase order.
An AQL value alone is incomplete. The inspection record should identify the lot size and boundaries, inspection level, normal/tightened/reduced status where applicable, sampling plan, sample size, defect classification, counting basis, and the applicable acceptance and rejection numbers. Use the agreed standard’s tables and switching rules; do not derive the acceptance count by multiplying sample size by the AQL percentage.
| Record | Minimum content | Decision control |
|---|---|---|
| Final sampling record | Order and lot; standard/edition; plan and level; sample selection; sample size; Ac/Re for each class; actual counts; report date | Compare counts using the agreed plan. Record the disposition of failures and the reinspection basis. |
| Performance-test record | Material/color/lot; specimen ID; method/edition; conditioning; test conditions; acceptance limit; measured result; report reference | A report must cover the relevant product and requirement. Missing, failed or mismatched evidence remains an open item. |
| Release record | Accepted quantity; packing-list revision; open holds; concession references; approver and date | A passed sampled inspection does not by itself authorize dispatch if other release requirements remain unresolved. |
Sampling can support a lot decision, but it cannot guarantee that every unit is defect-free. Keep laboratory testing, workmanship sampling and shipment authorization distinguishable in the file. Each answers a different question and may involve a different approval owner.
Which Records Should a Buyer Request?
The strongest quality file is compact and traceable. Request records that prove the order passed its specified gates rather than collecting unrelated certificates.
Material file
- Approved swatches and component list
- Fabric lot and roll identity
- Incoming inspection results
- Applicable lab or mill reports
Sample file
- Current tech pack and measurement chart
- Revision history and fit comments
- Approved artwork and placement
- Final approval evidence
Production file
- First-piece and in-line checks
- Nonconformity and corrective-action logs
- Bulk measurement results
- Rework and recheck evidence
Release file
- Final inspection report
- Quantity, SKU and packing verification
- Required performance-test results
- Shipment release or approved concession
What Buyers Must Define Before Ohsure Starts
- Technical baseline: provide a controlled tech pack, measurement method, tolerances and artwork files.
- Performance claims: identify every claim that needs a test and the destination-market requirement.
- Approval authority: name who may approve materials, samples, deviations and shipment.
- Defect language: define critical, major and minor defects with visual examples when possible.
- Inspection plan: state checkpoints, sample size or frequency, acceptance rules and reporting format.
- Change control: require written approval before substituting a fabric, trim, process or production site.
A buyer can use the Ohsure factory verification hub, factory overview, capacity methodology and certification evidence guide as related due-diligence context.
Download the QC Handover and Release Forms
Download the 14-point checklist and blank inspection records. Save the HTML file and open it in a browser to print or save as PDF. The forms include a sampling/test record and a corrective-action/reinspection log.
For sampling principles and the wider inspection programme, see the activewear quality-control guide. For project sequencing, read the inquiry-to-delivery process.
Frequently Asked Questions
These questions address common approval decisions; they are editorial guidance, not a quotation of customer inquiry records.
Does an approved sample guarantee bulk quality?
No. It defines a reference, but bulk quality also depends on matching materials, controlled patterns and artwork, stable production processes, in-line checks and a documented final release.
Should every fabric test be run on every order?
Not automatically. Select tests according to material, garment use, marketing claims, buyer requirements and destination regulations. Record which color and lot the result covers.
What happens if bulk material differs from the sample?
Stop the affected process, identify the difference, assess its impact and obtain written buyer disposition. Do not treat an unapproved substitution as equivalent because the composition name looks similar.
Is final inspection enough for activewear?
No. Final inspection may find visible or measurable defects, but it is less efficient at correcting fabric, cutting, print or sewing problems already repeated across the lot.
Can a buyer appoint a third-party inspector?
Yes, if the purchase terms grant access and define timing, lot readiness, standards, reporting and responsibility for failed or delayed inspections.
What is the most important QC document?
There is no single document. The essential chain is the approved specification and sample, material identity, process inspection records, corrective actions and the final release tied to the same purchase order.
Build a Traceable Order Quality File
Ohsurewear publicly describes quality control from fabric receipt through finished-garment inspection. Buyers can make that process auditable by defining each quality gate before the order begins, linking evidence to the actual material lot and style, closing deviations in writing, and preventing the next stage from starting until the required approval is complete.
Sources and Scope
Company process descriptions: Ohsure quality control and sportswear manufacturing. Sampling reference: ISO 2859-1:2026. Reviewed October 7, 2026. The proposed responsibility matrix and downloadable records are buyer tools; no order-specific test results, factory pass rates or signed release records have been supplied for this article.